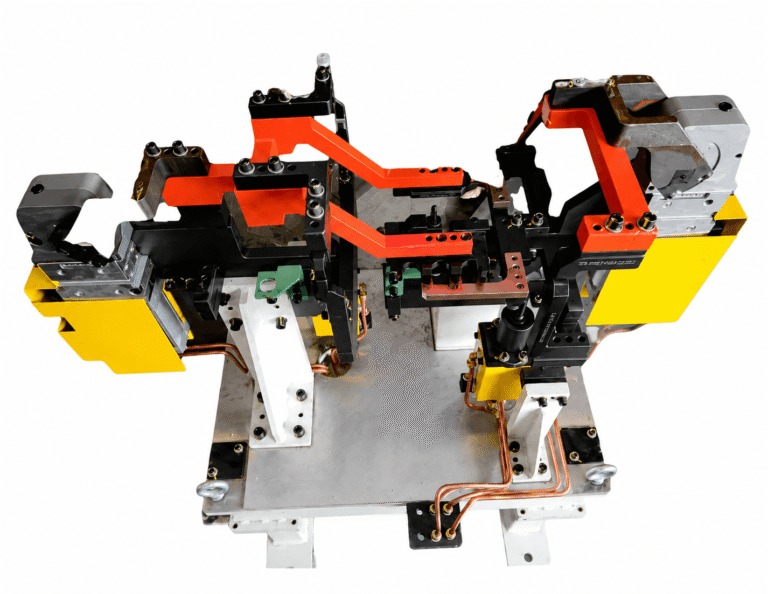
Jigs And Fixtures
₹115,000.00
Custom jigs and fixtures for machining, assembly, welding and inspection, engineered around your component drawing.
A jig guides the cutting tool as well as holding the work; a fixture only locates and clamps it. VR Automation designs and manufactures drill jigs, CNC and VMC workholding fixtures, assembly fixtures, checking fixtures, relation gauges and drill gauges at Bhosari, Pune, for automotive and precision engineering manufacturers.
The terms get used loosely, but the difference decides how the tooling is designed. A jig both holds the component and guides the tool, typically through hardened drill bushes, so accuracy of the hole comes from the jig rather than from the machine. A fixture holds and locates the component relative to the machine, and accuracy comes from the machine’s own axes. Drill jigs are the classic jig; VMC and CNC workholding is almost always a fixture.
Every fixture starts from a datum scheme. The standard approach constrains all six degrees of freedom through a 3-2-1 location: three points define the primary plane, two define the secondary, one the tertiary. Add more locating points than the scheme requires and the part becomes over-constrained — it will sit differently depending on clamping order, and repeatability is lost. Where a component is flexible or formed, we use nett-form locators and supports that take up variation without forcing the part into a shape it will not hold once released.
The second rule is that fixture datums must match inspection datums. A fixture located from features the CMM does not use will produce parts that measure out of tolerance even when the process is capable.
| Category | Purpose |
|---|---|
| Drill jigs and drill bush plates | Guide the drill to position without marking out; plate, box and leaf jig styles |
| CNC / VMC workholding fixtures | Locate and clamp for machining; single and multi-part layouts to fill the table |
| Hydraulic and pneumatic clamping fixtures | Fast, repeatable, sequence-controlled clamping for production volumes |
| Assembly fixtures | Hold components in relative position during riveting, screwing, pressing or bonding |
| Riveting machine fixtures | Locate the component under the riveting head and index it between rivet positions |
| Checking fixtures and relation gauges | Verify form, position and relationship between features against the drawing datum scheme |
| Drill gauges and inspection gauges | Go/no-go and positional verification of drilled and formed features |
A checking fixture is inspection tooling, and it is held to a tighter standard than production tooling because the measurement is only as good as the fixture. Ours are built to the component’s drawing datum scheme, with locators and supports representing the datums exactly, and with go/no-go pins, profile blades or dial indicators at the checked features. Where a customer requires it, the fixture is supplied with a gauge R&R study or a CMM-verified certification report so it can be entered into a calibration schedule.
Relation gauges verify not a single dimension but the relationship between features — hole-to-hole position, flange-to-face relationship, profile against a datum — which is precisely what a hand measurement cannot do repeatably on a formed part.
Related: welding and robotic fixtures, riveting machines.
₹115,000.00
Custom jigs and fixtures for machining, assembly, welding and inspection, engineered around your component drawing.
₹70,000.00
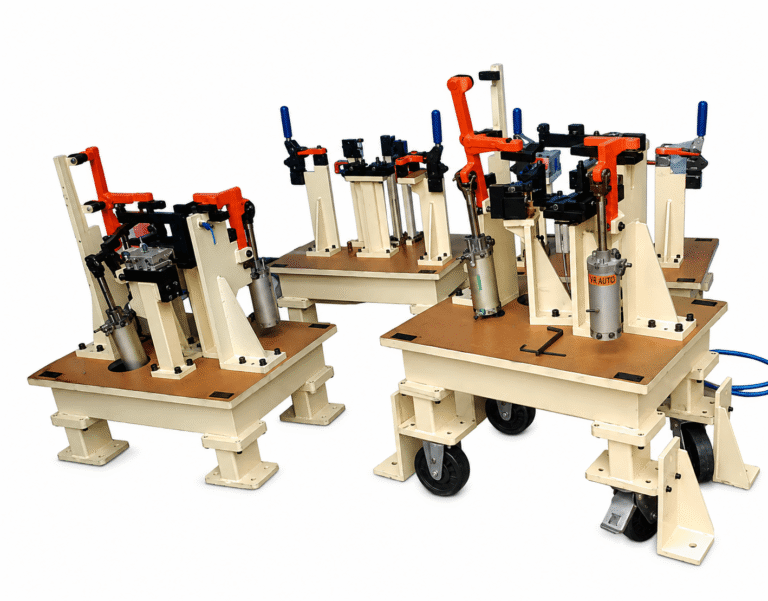
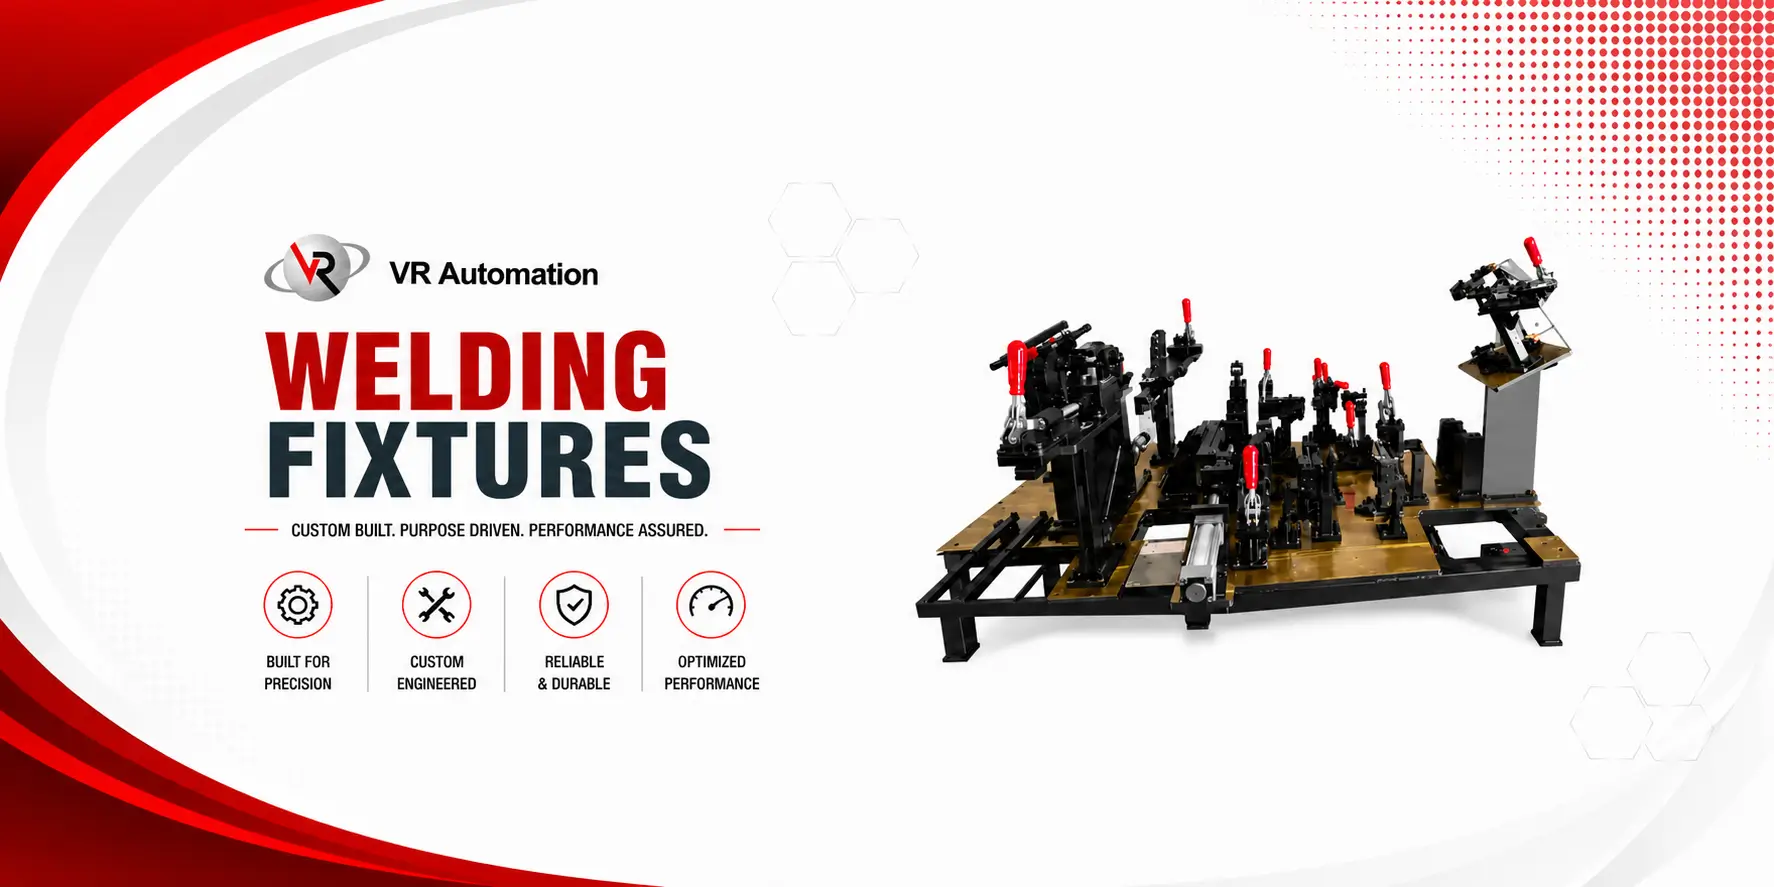
Welding jigs and fixtures that locate and clamp components accurately and hold them square against weld distortion.
₹15,000.00
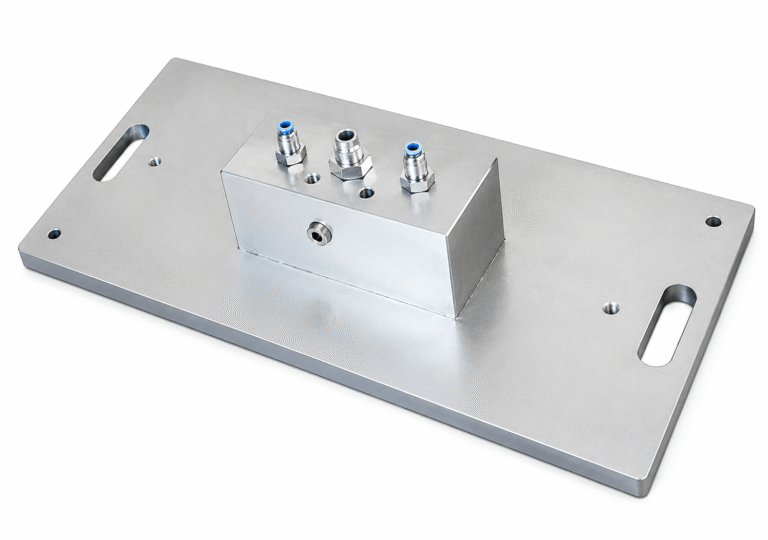
Riveting machine fixtures are used to position and rotate a fixture to set rivets at specific locations. They can be…
₹9,000.00
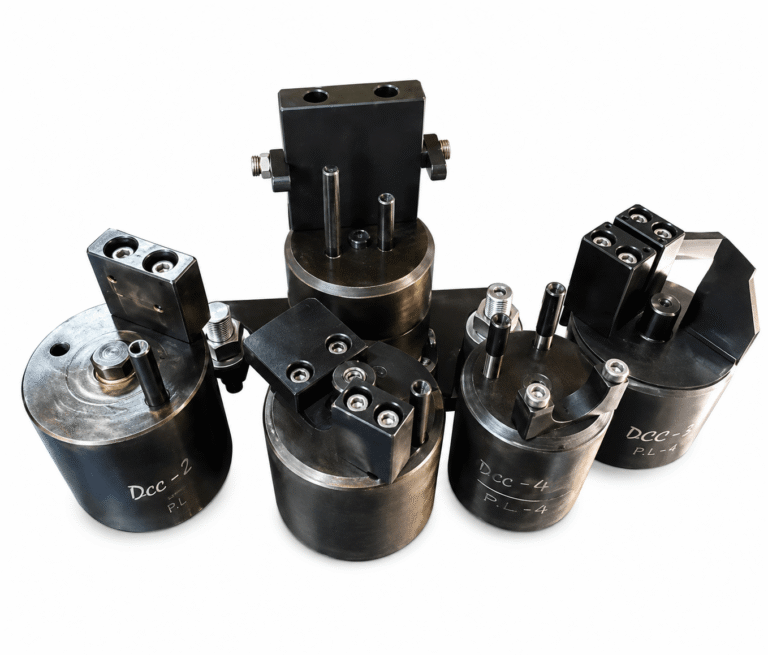
Component fixtures for riveting machines, locating the part accurately and repeatably beneath the riveting head.
₹25,001.00
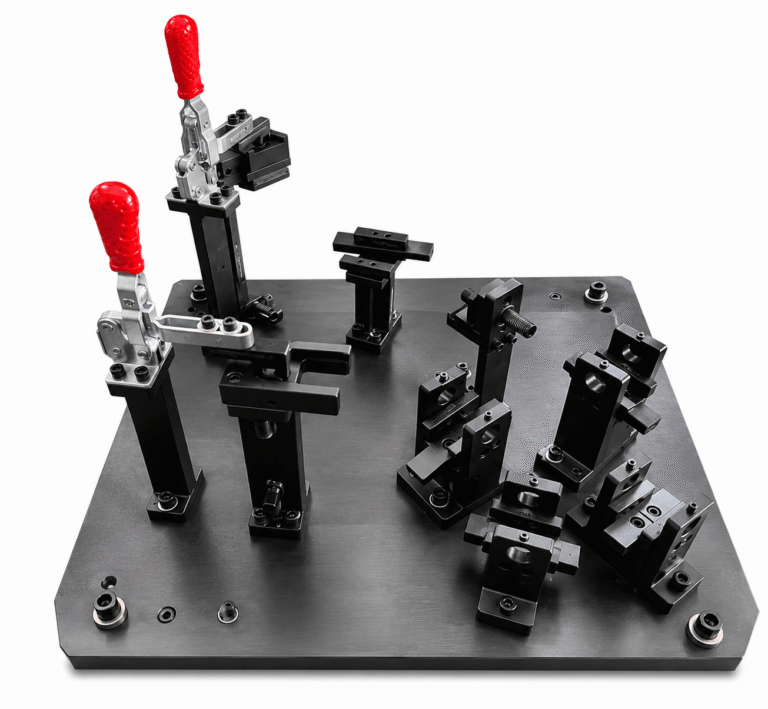
Inspection fixtures and relation gauges for quick go/no-go dimensional checks at the point of manufacture.
₹18,000.00
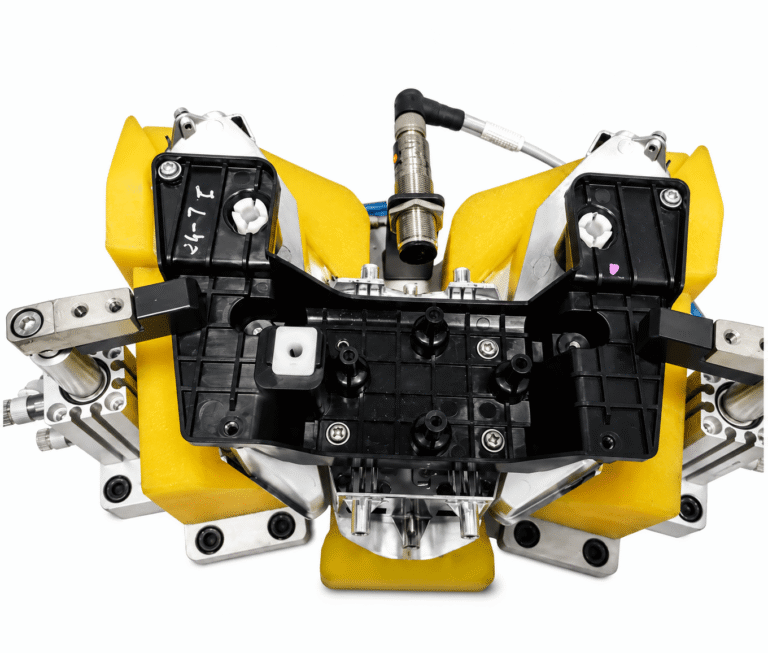
Component fixtures for screw driving stations, locating each screw position accurately under the driver.
A jig holds the component and also guides the cutting tool, usually through hardened drill bushes, so positional accuracy comes from the jig. A fixture only locates and clamps the component relative to the machine, and accuracy comes from the machine axes. Drill jigs are jigs; VMC workholding and assembly tooling are fixtures.
A relation gauge is an inspection fixture that verifies the relationship between features — hole-to-hole position, profile against a datum face, flange orientation — rather than a single isolated dimension. It is used where a formed or fabricated part cannot be checked repeatably with hand instruments.
Our fixtures currently start from around ₹9,000 for a simple riveting machine fixture and ₹25,000 for an inspection fixture with relation gauges, rising with part complexity, clamping type and certification requirements. Send the component drawing with the datum scheme for a firm quotation.
Yes, on request. Checking fixtures and gauges can be supplied with CMM verification against the drawing datum scheme and a gauge repeatability and reproducibility study, so they can be entered directly into your calibration system.
Yes. Formed parts need nett-form locators and compliant supports that take up part variation without forcing the component into a shape it will not hold when released, and a clamping sequence designed so the part is not distorted by the act of clamping. This is a core part of our fixture design work.
VR Automation, Bhosari, Pune — riveting, clinching, press and special purpose machines. We quote against your part, not a catalogue.
These products are limited, checkout within
Riveting, clinching, press & SPM machines — built in-house at Bhosari, Pune. Supplied PAN India since 2019.
Tell us about your component and joint. We quote against your part, not a catalogue.