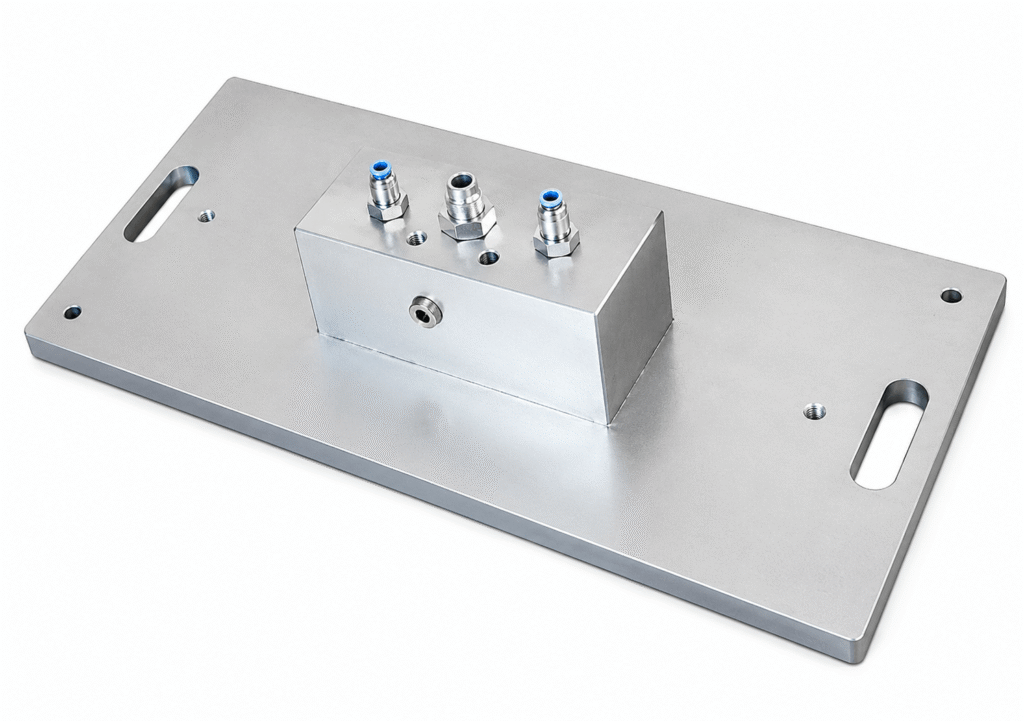
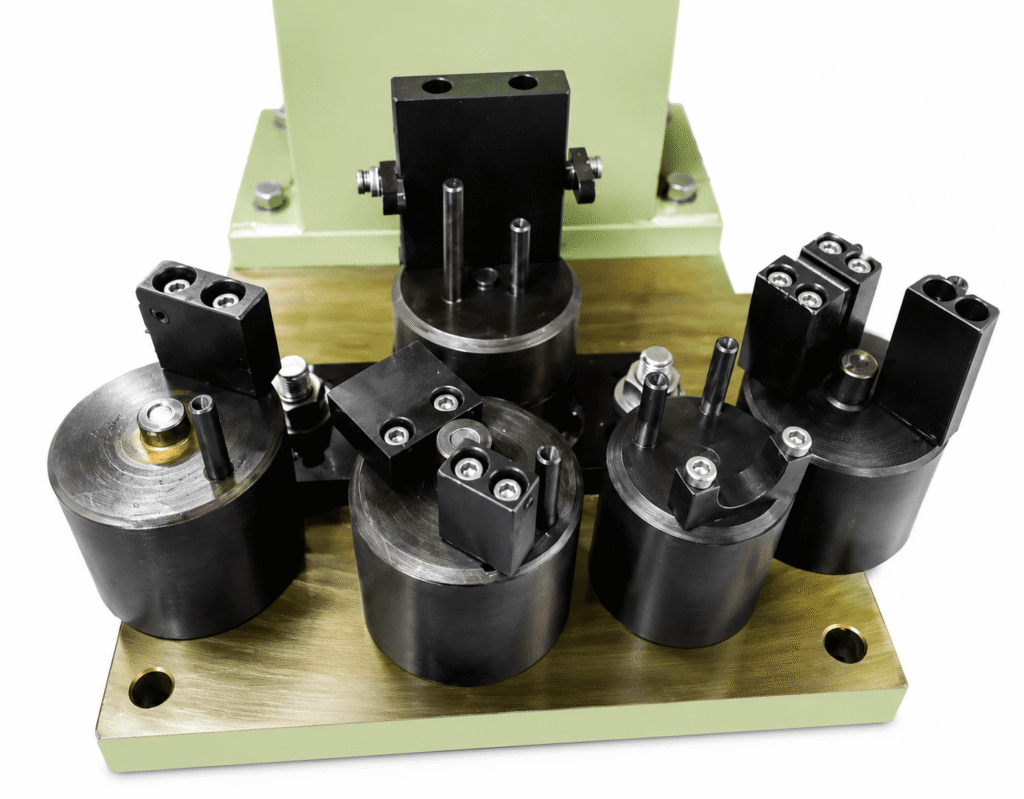
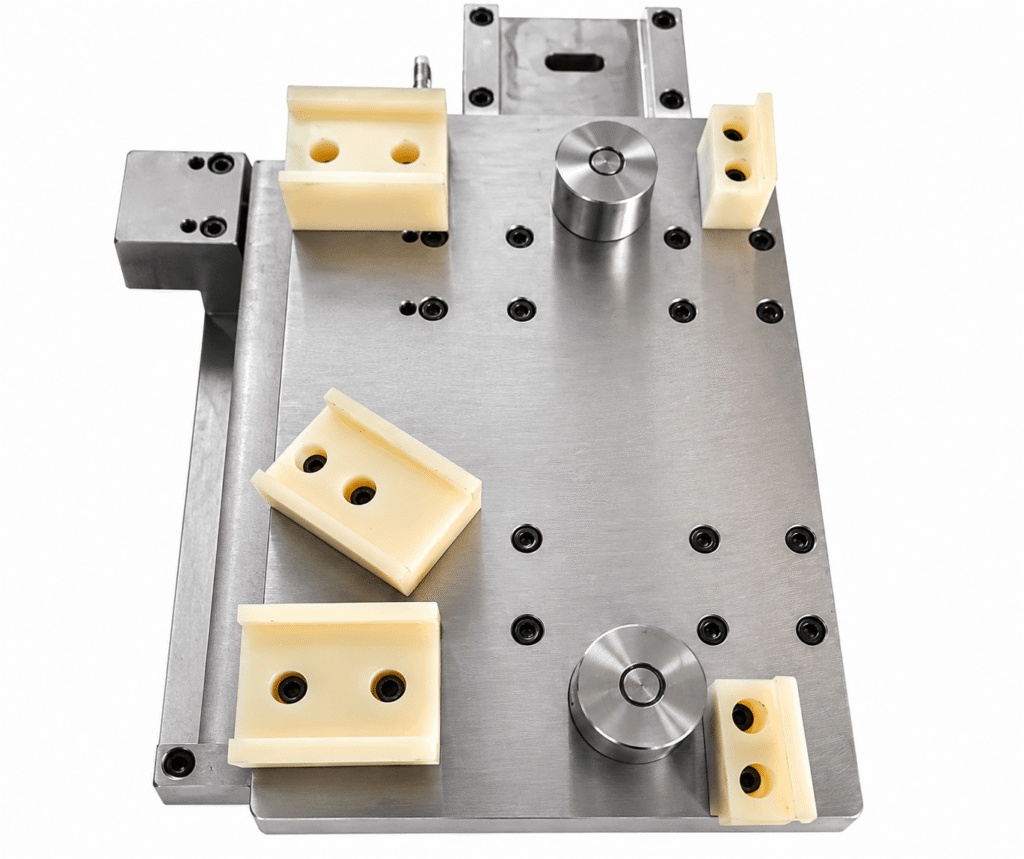
Riveting Machine Fixtures
| Fixture Type | Riveting Locating Fixture |
| Clamping Type | Manual |
| Machine Compatibility | Riveting Machine |
| Material | Mild Steel |
| Surface Finishing | Coated |
| Type | Broaching |
| Max Workpiece Size | 301-600 mm |
| Max Clamping Force | 11-20 kN |
| Fixture Type | Riveting Locating Fixture |
| Clamping Type | Manual |
| Machine Compatibility | Riveting Machine |
| Material | Mild Steel |
| Surface Finishing | Coated |
| Type | Broaching |
| Max Workpiece Size | 301-600 mm |
| Max Clamping Force | 11-20 kN |
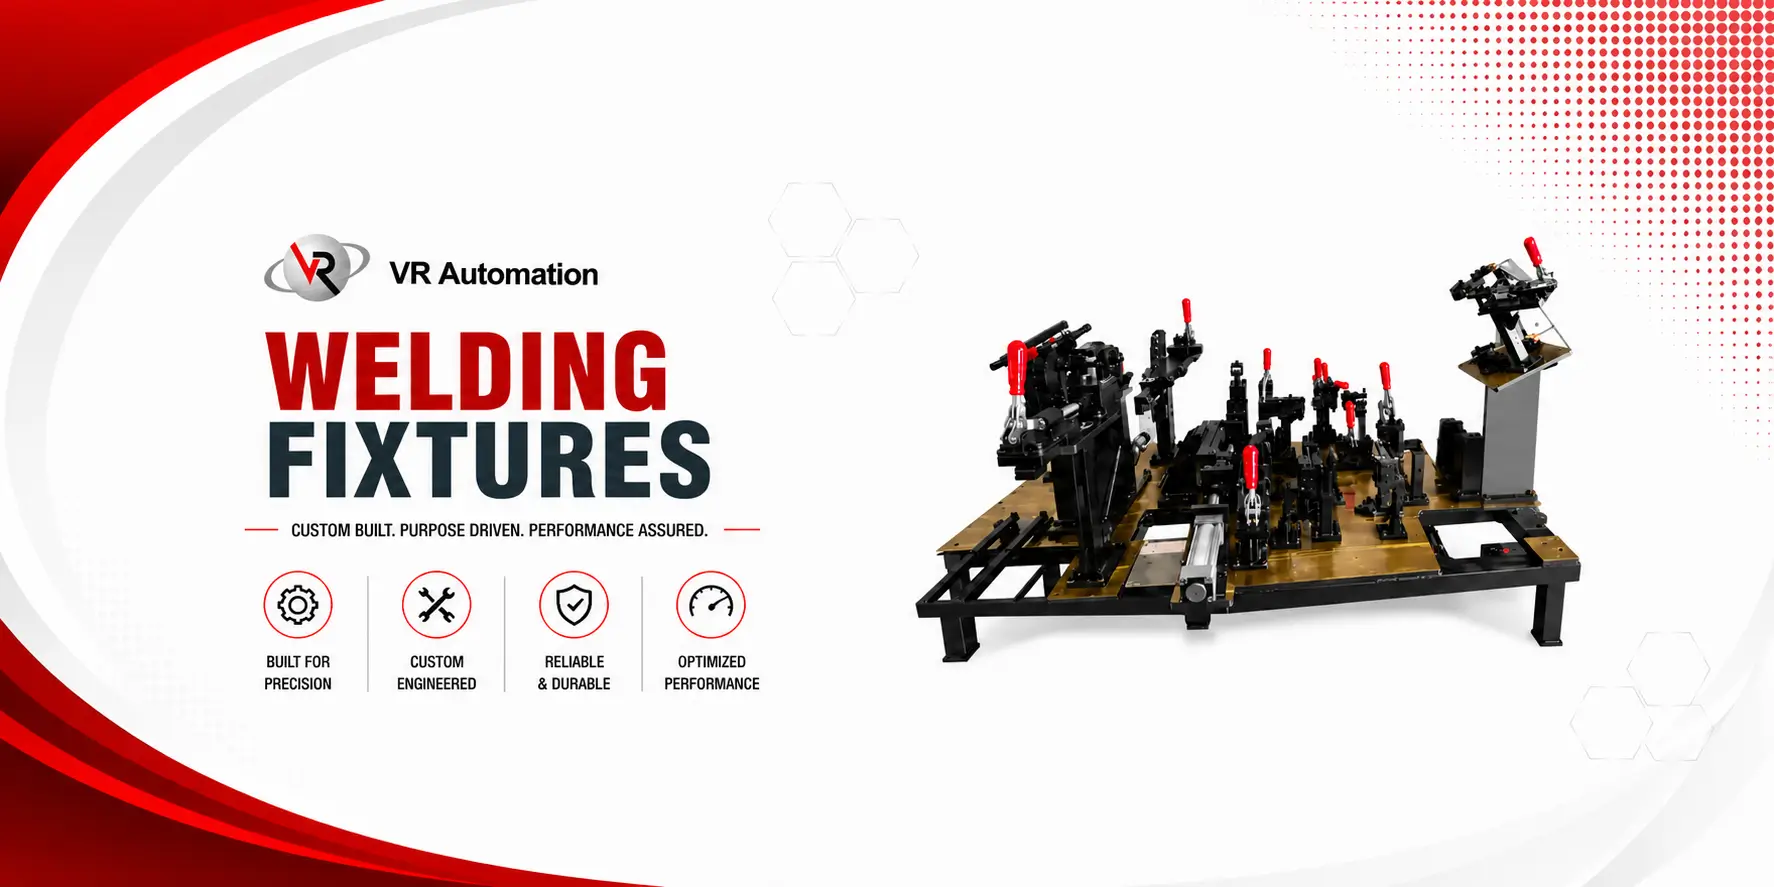
Riveting fixtures for components carrying several rivets, where each position must be located and the part indexed between them. The fixture holds the relationship between rivet positions that the operator otherwise has to judge.
By indexing the part against positive stops within the fixture, so the relationship is set by the tooling rather than by the operator repositioning the work each time.
It is the lower cost route. A multi-head machine sets the rivets simultaneously and is faster; an indexed fixture sets them in sequence on a single head. Volume and cycle time decide which is justified.
Generally yes, given the machine table and tool holder details plus the component drawing.
Send us the component drawing and joint specification. VR Automation quotes against your part, not a catalogue.
These products are limited, checkout within
Tell us about your component and joint. We quote against your part, not a catalogue.