Crimping Machine Tool
₹45,000.00
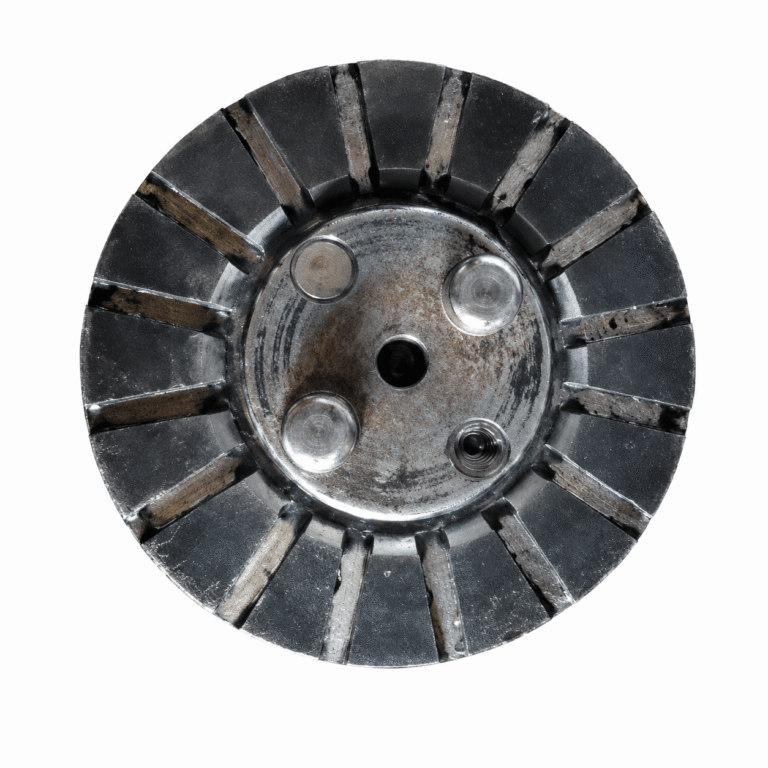
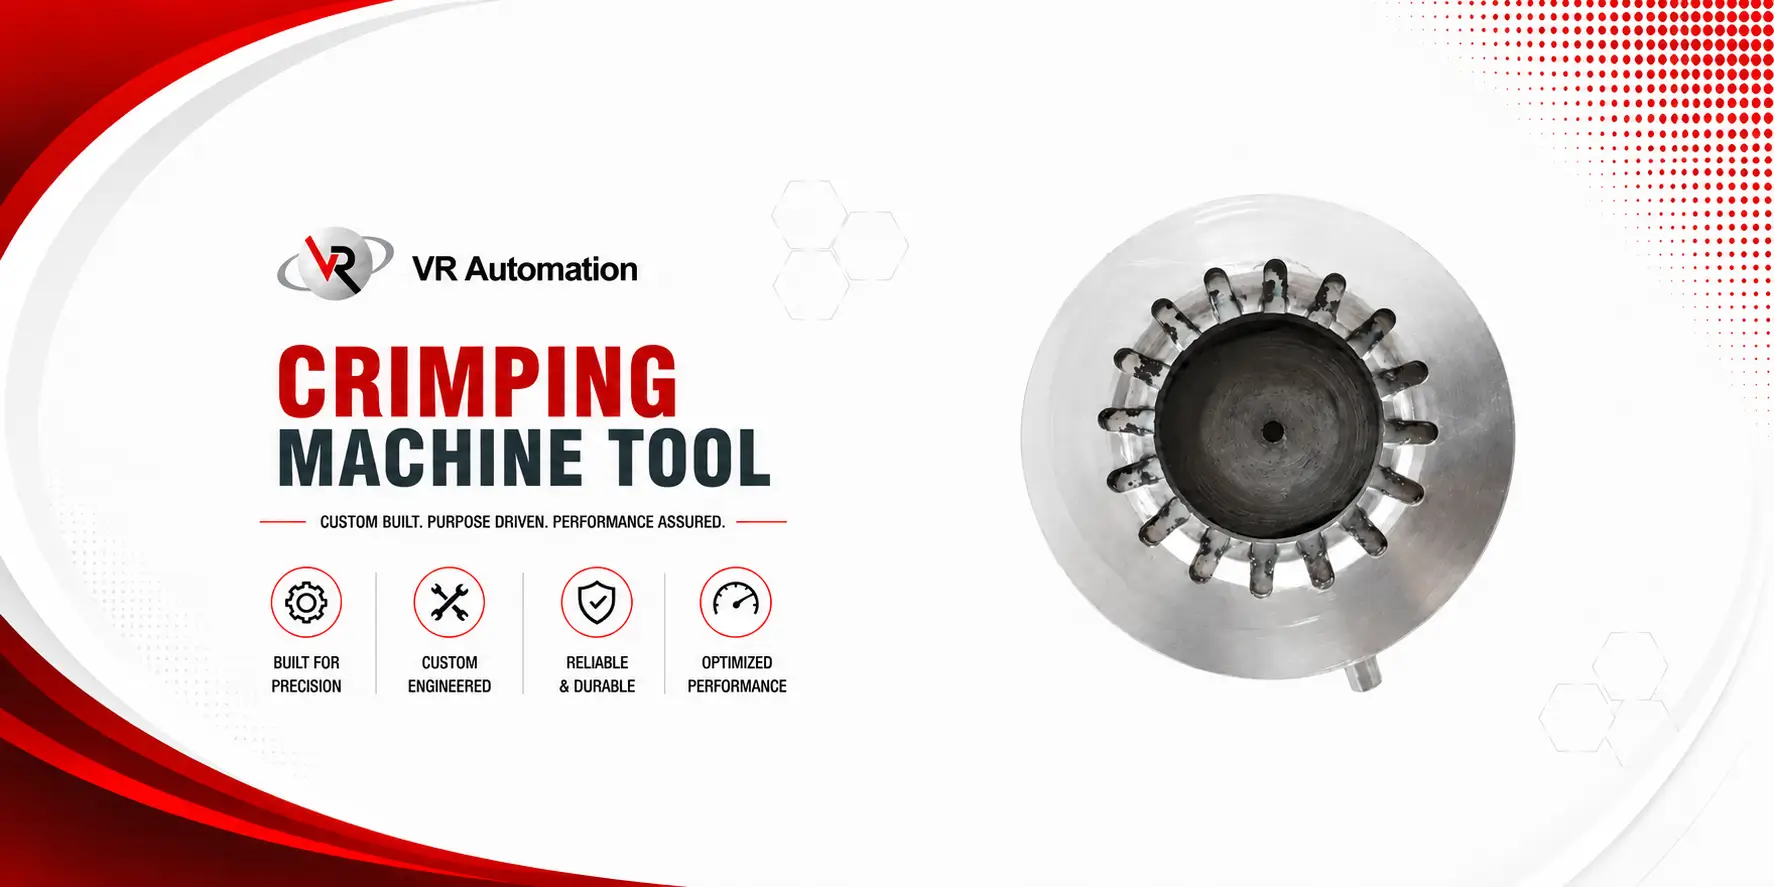
Crimping machine and tooling producing consistent, gas-tight crimped joints with repeatable compression on every cycle.
A terminal crimping machine forms a gas-tight mechanical and electrical joint between a wire and a terminal by compressing the terminal barrel around the conductor with a matched applicator die. VR Automation builds pneumatic and hydraulic crimping machine tools, cable lug crimpers and wire harness crimping stations at Bhosari, Pune.
A correct crimp is not simply a squeezed terminal. The barrel is deformed until the conductor strands cold-weld against each other and against the barrel wall, eliminating the air gaps where oxidation and corrosion would otherwise start. That is what “gas-tight” means, and it is why a properly crimped joint outperforms a soldered one under vibration.
Three measurements govern it, and every crimping machine specification comes back to them:
| Format | Actuation | Typical work |
|---|---|---|
| Benchtop terminal crimping press | Pneumatic or electric | Harness shops, low to medium volume, applicator changeover between jobs |
| Pneumatic terminal crimper | Air cylinder, foot pedal | General terminal and ferrule crimping in panel and harness assembly |
| Hydraulic / hydro-pneumatic cable lug crimper | Air-over-oil booster | Heavy battery cables, copper lugs, thimbles, hexagon and indent crimps |
| Semi-automatic crimping machine | Powered with manual wire loading | Repetitive terminal application where the operator still positions the wire |
| Automatic wire stripping and crimping machine | Fully automated cycle | High-volume harness production; cut, strip, crimp in one sequence |
| Hose crimping machine | Hydraulic, segmented die | Hydraulic hose and fitting assembly — a different process from wire crimping |
The press supplies force; the applicator and its die set decide the crimp. Applicators are specific to the terminal — its series, its barrel size and whether it is supplied loose-piece or on a reel — so a machine tooled for one terminal will not crimp another correctly regardless of how the press is set. When specifying a crimping machine, the terminal part number and the wire gauge range matter more than the tonnage.
Die sets for lug and thimble crimping follow the same logic: hexagon dies for compression lugs, indent dies for certain connector types, and each sized to the conductor cross-section in sq mm.
Automotive wire harness manufacture, EV harness and battery cable assembly, switchgear and control panel wiring, appliance and motor lead assembly, solar DC cabling, and electrical contractor workshops making up lugs and thimbles on site.
Related: hydro-pneumatic presses, tooling and die sets, screw driving automation.
₹45,000.00
Crimping machine and tooling producing consistent, gas-tight crimped joints with repeatable compression on every cycle.
₹125,000.00
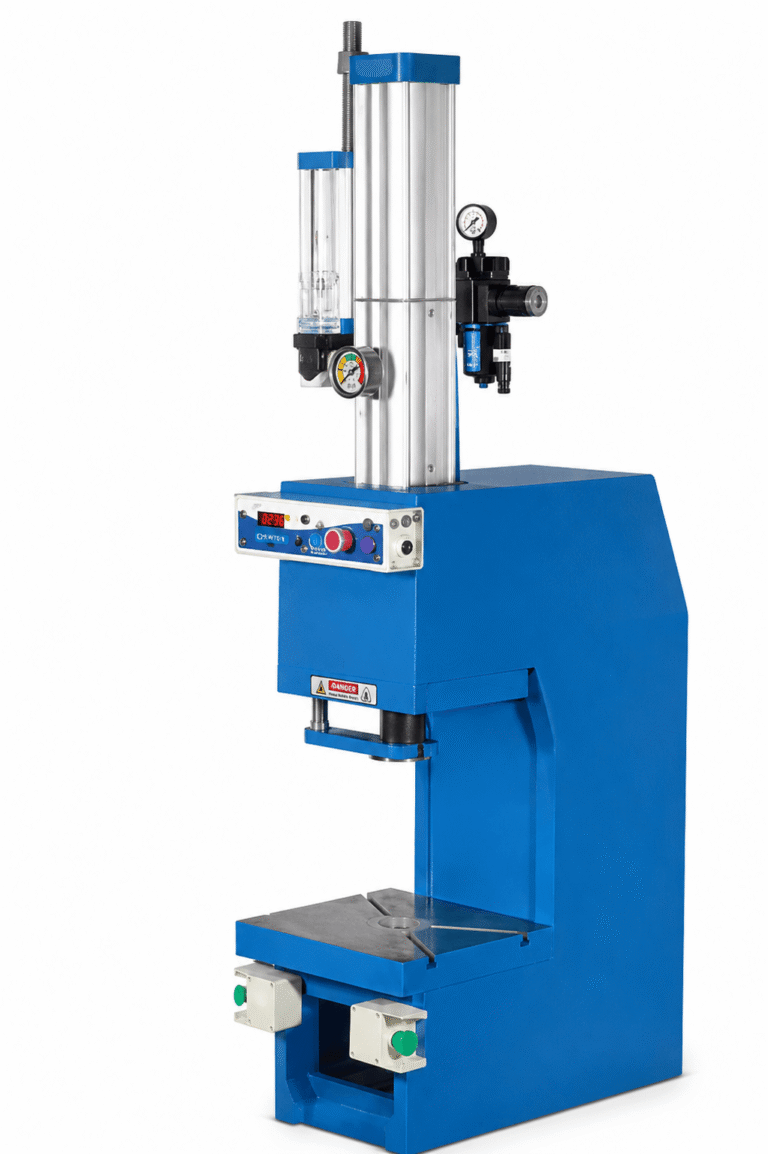
Compressed-air press for pressing, staking, marking and light forming, with fast cycling and low running cost.
₹175,000.00
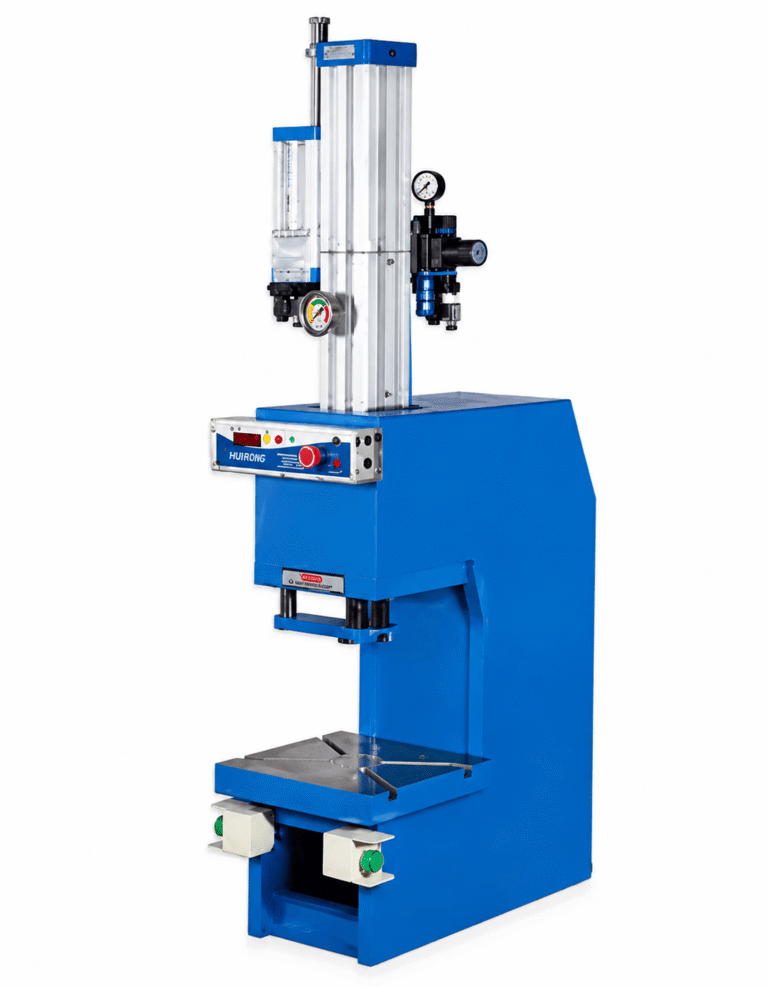
Air-over-oil press delivering high force from a standard compressed air supply, with no hydraulic power pack required.
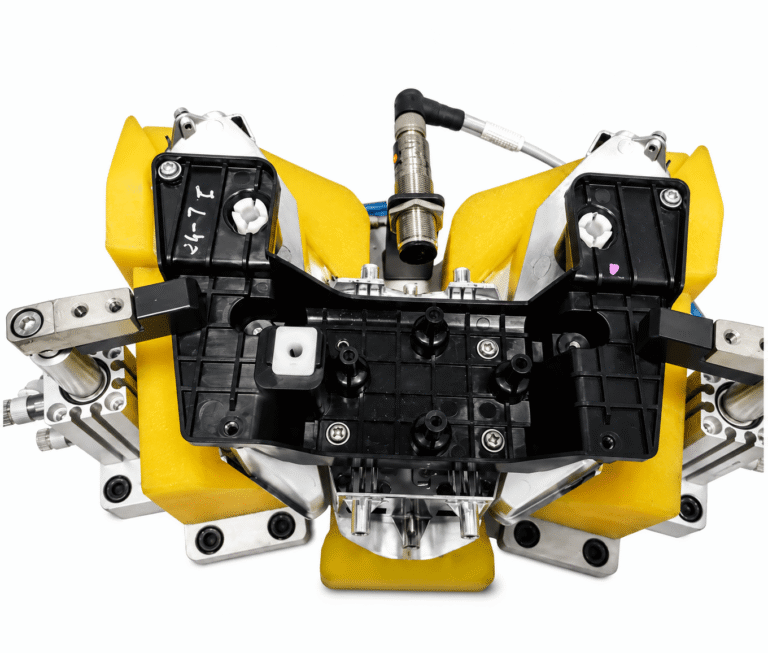
₹18,000.00
Component fixtures for screw driving stations, locating each screw position accurately under the driver.
VR Automation crimping machine tools are currently listed from about ₹45,000. Price depends on force class, whether actuation is pneumatic or hydro-pneumatic, and on the applicator or die set required — tooling is terminal-specific and is quoted against your terminal part number.
Crimp height is the finished height of the crimped terminal barrel, measured with a crimp height micrometer. It is the primary control dimension in harness manufacture: too high and the strands are not compacted enough to be gas-tight; too low and the strands are cut, reducing pull-off force. Terminal manufacturers publish a target and tolerance for every wire gauge.
They share a name and little else. A wire crimping machine compresses a terminal barrel onto electrical conductors using a flat or indent applicator die, typically at low tonnage. A hose crimping machine closes a ring of segmented dies radially around a hydraulic hose ferrule at high force. The tooling, force class and control requirements are entirely different.
Yes, in almost all cases. The applicator is matched to the terminal series and barrel size, and whether the terminal is supplied loose-piece or on a reel. This is why we ask for the terminal part number before quoting, rather than only the required tonnage.
Yes, where the application demands it. Force-and-displacement monitoring across the crimp stroke produces a signature curve that detects a missing strand, an under-inserted wire or a worn applicator, and can be logged per crimp. This is increasingly required in EV and safety-critical harness manufacture.
VR Automation, Bhosari, Pune — riveting, clinching, press and special purpose machines. We quote against your part, not a catalogue.
These products are limited, checkout within
Riveting, clinching, press & SPM machines — built in-house at Bhosari, Pune. Supplied PAN India since 2019.
Tell us about your component and joint. We quote against your part, not a catalogue.